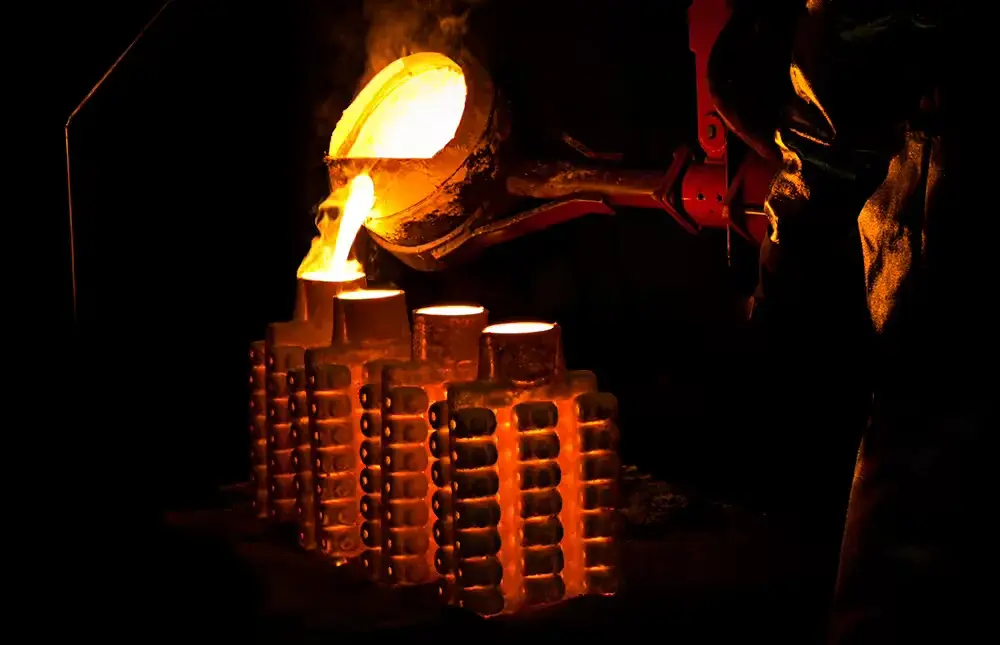
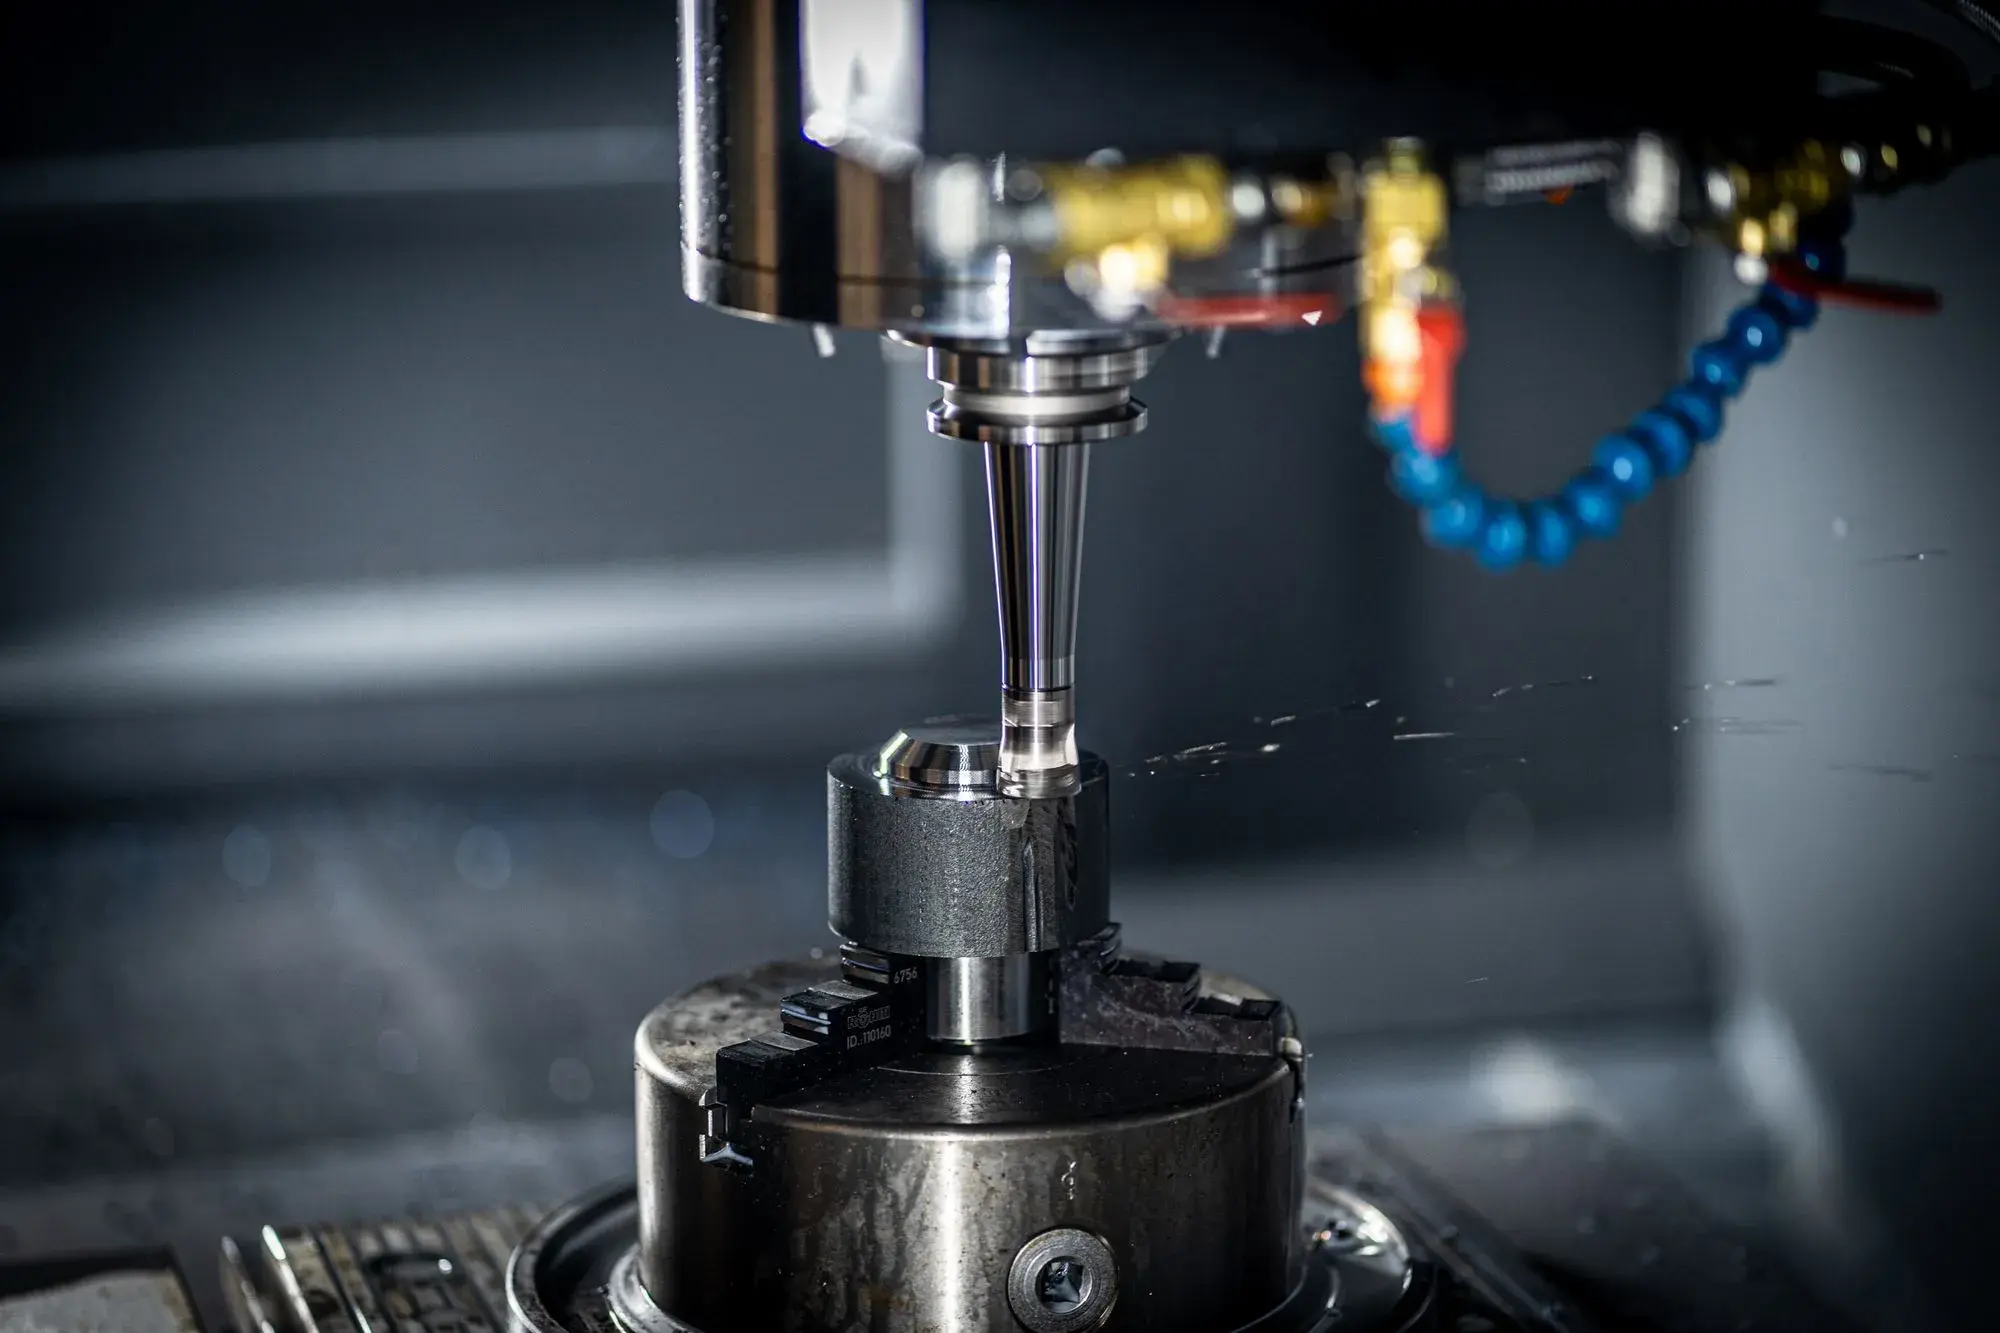
A casting that is easy to machine is quicker to produce, more consistent and cheaper. Most of those savings are decided on the drawing, long before metal is poured.
Define datum features
Give the machinist clear, cast-in datum surfaces that locate the part repeatably in a fixture. Avoid placing datums on parting lines or gate locations.
Allow the right machining stock
Investment castings need far less stock than sand castings — often 0.5 to 1 mm on critical faces. Too much stock wastes cycle time; too little risks clean-up problems.
Cast and machine with one supplier
When the same team casts and machines a part, tooling, fixtures and tolerances are planned together. That is how Godani delivers finished, ready-to-fit components.